Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
Choosing the 2026 best 200*1800mm Graphite Electrode requires more than comparing prices or catalog photographs. This compact format may suit small electric arc furnaces, ladle furnaces, and specialized melting operations. However, the correct type depends on furnace capacity, transformer power, operating current, and steel grade.
Common options include regular power (RP), high power (HP), and ultra-high power (UHP) graphite electrodes. RP electrodes can fit moderate workloads and cost-sensitive projects. HP designs provide better current tolerance and thermal stability. UHP electrodes usually support demanding furnace cycles, but their higher price needs technical justification. Check resistivity, bulk density, ash content, flexural strength, and thermal expansion before ordering.
A reliable supplier should provide batch traceability, dimensional inspection, test reports, and nipple specifications. Confirm the actual diameter, length, machining tolerance, and joint design. Small differences can affect electrode alignment and consumption. Storage also matters. Keep electrodes dry, covered, and separated from chemicals or impact risks.
Real operating data matters most.
A buyer may select UHP material too quickly. That choice can waste money when furnace power remains limited. Conversely, a low-grade electrode may crack during rapid heating or unstable current conditions. This is where practical experience becomes valuable. Compare supplier records, independent test results, and your furnace history. No single type is best for every plant. The best 200x1800mm Graphite Electrode is the one that matches measurable operating demands, verified quality, and realistic maintenance conditions. Expect careful review, not a perfect shortcut.
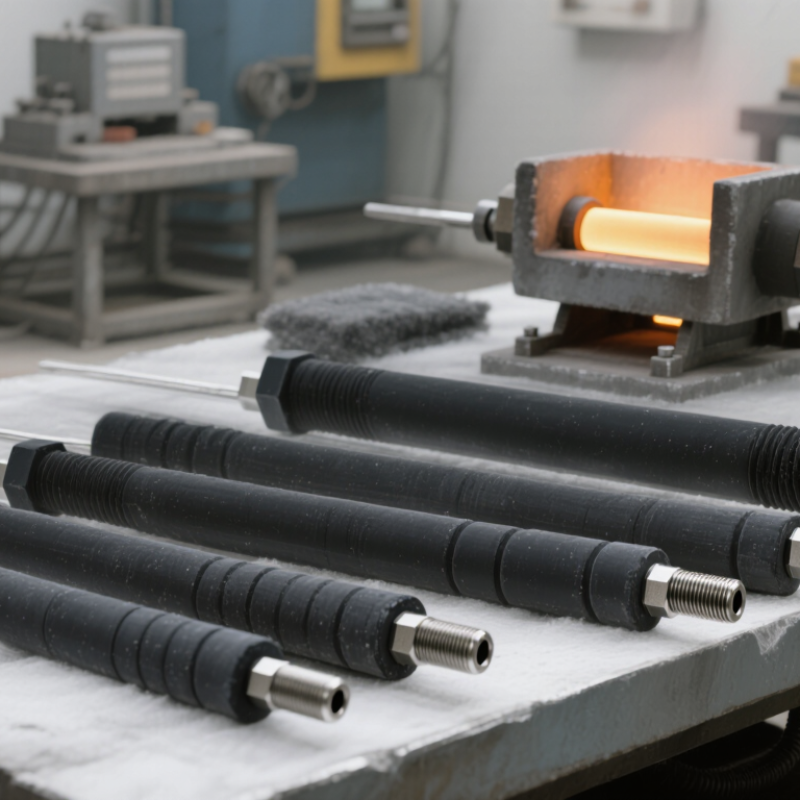
For 200×1800 mm graphite electrodes, grade selection should follow furnace load, current density, and operating temperature. Regular Power (RP) grades suit lighter electrical demands. High Power (HP) grades handle greater current with improved thermal resistance. Ultra-High Power (UHP) grades provide the lowest electrical resistivity, but they are not automatically the best choice for every furnace.
The stated dimensions mean a nominal diameter of 200 mm and a nominal length of 1800 mm. Actual measurements need agreed tolerances. Check diameter at several points, because machining marks or local wear can affect readings. Inspect the end faces carefully. They should remain flat, clean, and free from deep cracks. Thread dimensions must match the selected nipple system, including pitch, taper, and engagement depth.
Standards should define test methods for resistivity, bulk density, flexural strength, and thermal expansion. Purchase specifications may reference ASTM or ISO procedures, but the exact method must be written clearly. In practical inspections, packaging damage is easy to overlook. It can later become a breakage risk during connection. A lower-resistivity electrode may reduce voltage loss, yet grade data alone cannot predict furnace performance. I would recheck the current rating and connection design before approval. Dimensions are simple. Compatibility is not.
For a 200×1800 mm graphite electrode, diameter matters more than length when selecting operating current. The 200 mm section provides about 314 cm² of conducting area. Industry technical tables commonly place RP resistivity near 8.5 μΩ·m, HP near 6.5 μΩ·m, and UHP near 5.5 μΩ·m. Lower resistivity means less voltage loss and less heat generated inside the electrode. These figures are typical ranges, not guarantees. IEC 60239 provides the terminology and testing framework, but furnace conditions still change real performance.
Current density separates the three grades more clearly. RP is often used around 14–22 A/cm², equivalent to roughly 4,400–6,900 A for this diameter. HP commonly operates near 18–28 A/cm², or about 5,700–8,800 A. UHP may reach 25–35 A/cm², giving approximately 7,900–11,000 A when cooling and power control are adequate. A 2024 industrial graphite market review linked rising electric-arc-furnace output with stronger demand for high-current electrodes. USGS Mineral Commodity Summaries 2024 also identified graphite as a critical industrial material, although it does not publish electrode-grade limits. Field experience suggests that UHP is not automatically better. Poor nipple contact, unstable charging, or uneven cooling can erase its advantage. The uncomfortable detail is simple: a lower-resistivity electrode can still fail early when the furnace setup is poorly matched.
For high-power EAFs, a 200mm UHP graphite electrode must match the furnace’s real electrical load. Its cross-sectional area is about 314cm². At 25–35 A/cm², the operating current reaches approximately 7,850–11,000 amperes. This range is demanding, not decorative.
Choose UHP material with low electrical resistivity, low thermal expansion, and consistent bulk density. These properties help reduce oxidation, thermal shock, and tip breakage during rapid melting. The 1,800mm length also affects column stability. Poor alignment can create side loading near the nipple connection. That failure often begins quietly.
Check the electrode’s measured resistance, diameter tolerance, nipple fit, and machining quality before installation. A clean joint matters. Dust, damaged threads, or uneven contact can increase local heating. Furnace power, arc length, cooling conditions, and scrap density must also support the target current density. A theoretical 35 A/cm² setting may become unstable in a poorly balanced furnace.
One calculation mistake can distort the selection. I would not choose solely from a catalog rating. Actual transformer output and consumption records deserve more attention. During operation, monitor electrode breakage, oxidation marks, joint temperature, and kilograms consumed per ton. The best 200x1800mm UHP type is the one that remains stable under measured furnace conditions, not merely the one carrying the highest advertised rating.
For a 200x1800 mm graphite electrode, grade selection should begin with measurable quality data. A resistivity of no more than 6.2 μΩ·m supports lower electrical losses during arc-furnace operation. Bulk density of at least 1.60 g/cm³ indicates a tighter structure, which can reduce gas penetration and mechanical damage. These values are screening targets, not complete proof of performance.
Common options include regular-power, high-power, and ultra-high-power electrodes. A 200 mm electrode often suits smaller furnaces or moderate current loads, but the correct type depends on furnace current, arc stability, and duty cycle. ISO 8006 provides dimensional and designation guidance, while ASTM C651 and ASTM C559 define recognized methods for resistivity and bulk-density testing. Ask for laboratory results from each production batch.
World Steel Association statistics show electric-arc-furnace steelmaking remains a significant global route, increasing demand for consistent electrode consumption data. USGS Mineral Commodity Summaries also identifies graphite supply and processing quality as important industrial concerns. In practical inspections, check nipple fit, machining marks, end-face flatness, and visible cracks. A dense electrode can still fail if its thermal-expansion behavior is poor. That is the uncomfortable part. Specifications alone cannot predict every furnace event. Keep the test records. Compare them with actual breakage, consumption, and current readings.
For a 200 × 1800 mm graphite electrode, the thread and nipple deserve more attention than the diameter alone. A 200 mm electrode can use a 3TPI or 4TPI connection, depending on the specified standard and furnace load. Never mix thread profiles. Measure pitch, major diameter, socket depth, and nipple length with calibrated gauges. A clean-looking nipple is not proof of a correct fit. Small thread damage can create local heating, resistance, and column failure.
The World Steel Association reported that electric arc furnaces produced about 28% of global crude steel in 2023. This supports continued demand for stable electrode connections. The USGS Mineral Commodity Summaries 2025 also identifies graphite as a critical industrial material, with performance strongly linked to purity, strength, and thermal behavior.
During a furnace-fit check, confirm the full 1800 mm length, holder clearance, electrode alignment, and connection torque. Check both ends, even when only one end enters service. That step is often skipped.
TIPS
Keep nipples dry and dust-free. Use the approved thread gauge, not visual judgment. Check for chipped edges, oval sockets, and uneven contact marks. Leave clearance for thermal expansion. A connection that feels tight by hand may still be wrong. Recheck the procedure when field measurements disagree with the drawing; the drawing may be outdated, but the furnace will expose the error.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift