Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
Choosing among the 2026 Top Organic Fertilizer Processing Plant Suppliers requires more than comparing catalog prices. An Organic Fertilizer Processing Plant must match the feedstock, production target, and local operating conditions. Chicken manure, compost, sludge-free plant residues, and animal bedding behave differently during processing. Their moisture levels affect fermentation, crushing, granulation, drying, and screening. A reliable supplier explains these differences clearly. It should provide equipment layouts, energy estimates, material tests, and realistic capacity data. Numbers should be traceable.
The strongest suppliers usually support complete production lines, from raw material preparation to final bagging. Their systems may include compost turners, crushers, mixers, granulators, dryers, coolers, screens, and dust-control units. Pay attention to details. Can the granulator produce consistent particle sizes? Does the dryer protect nutrient quality? Are spare parts available near your market? Experienced engineers should also review drainage, ventilation, power supply, and workshop space before quoting. Site references and verified customer feedback add useful confidence. On-site trials matter.
No ranking can be perfect. Supplier performance may change with project scale, raw material quality, and after-sales support. Some quoted capacities remain conditional. That deserves careful review. This guide evaluates leading manufacturers through technical capability, practical experience, documentation, service responsiveness, and long-term operating value. Readers should request current certifications and independently verify test results. A cheaper line may become expensive when downtime, odor control, or replacement parts are ignored. The best decision is not always the largest plant. It is the system that performs reliably under your real conditions.
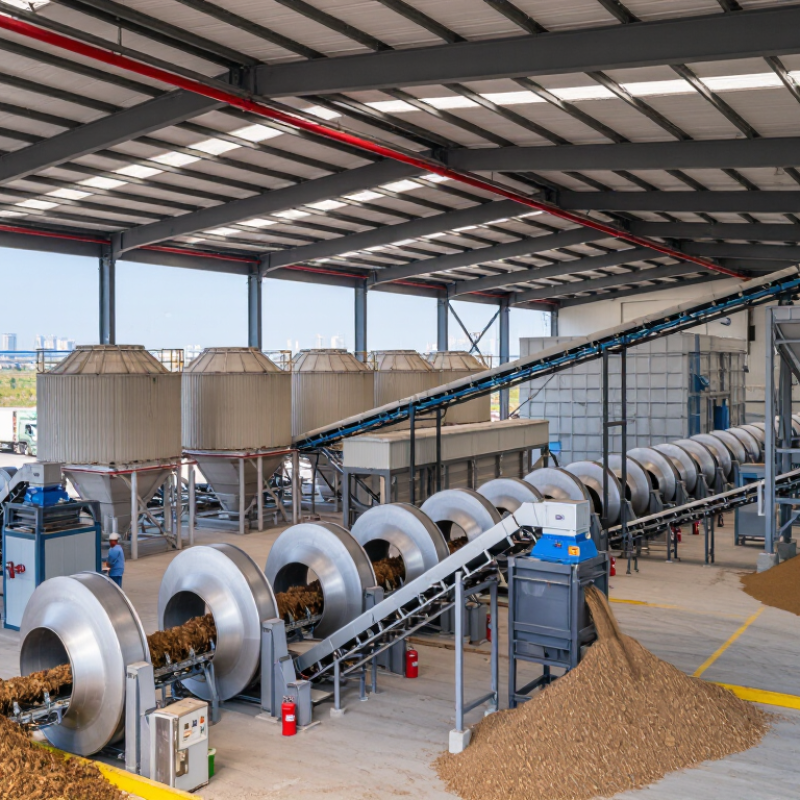
Organic fertilizer processing plants convert farm residues, livestock manure, and approved organic by-products into stable soil amendments. Their core function is controlled transformation, not simple mixing. A typical line may include shredding, blending, composting, drying, screening, and granulation. Each stage affects moisture, particle size, nutrient consistency, and storage life.
Experienced operators monitor temperature, oxygen, moisture, and odor during composting. A well-managed pile often feels warm and crumbly, rather than wet and compacted. Dryers reduce excess moisture, while screens remove stones and oversized fibers. Granulators then shape the material into uniform particles for easier spreading. Reliable plants also use sampling procedures to check nutrient levels, maturity, and unwanted contaminants. Still, no process is perfect. Feedstock changes with seasons, and one setting may not suit every batch.
Tips: Ask suppliers for process-flow drawings, capacity data, energy estimates, and maintenance requirements. Visit a working facility if possible. Watch how workers handle uneven feedstock, dust, and moisture changes. Confirm that safety controls and testing records are practical, not merely promised. A smaller plant with stable output can be more useful than a larger line that frequently stops. Pay attention to cleaning access. Neglected corners become problems.
In 2026, organic fertilizer plant suppliers must process variable feedstocks, not simply install larger machines. The UNEP Food Waste Index Report 2024 estimates that 1.05 billion tonnes of food were wasted in 2022. This creates a major feedstock opportunity, but contamination remains a practical problem. Effective plants use shredders, magnetic separators, and screening systems before biological treatment.
Aerobic composting depends on oxygen, moisture, and carbon balance. Forced-air tunnels can improve airflow through dense piles, while temperature sensors help maintain hygienic conditions. The process usually targets 55–65°C for pathogen reduction. However, heat alone is not enough. Operators must verify time, moisture, and uniform mixing. Poorly managed piles develop ammonia odors and uneven maturity.
Anaerobic digestion offers another route. It converts wet organic residues into biogas and digestate under oxygen-free conditions. The International Energy Agency identifies biogas and biomethane as important tools for recovering energy from organic waste. After digestion, screw presses or centrifuges separate solids and liquids. Low-temperature drying then reduces moisture for granulation, while rotary or disc granulators form consistent particles. The FAO’s work on soil fertility emphasizes the value of returning organic matter and nutrients to farmland, but nutrient content varies sharply by feedstock. That detail is often underestimated. A reliable plant therefore combines laboratory testing, batch traceability, dust control, and calibrated dosing equipment. Some designs still overpromise automation; human inspection remains necessary.
Supplier evaluation should begin with verified process evidence, not polished brochures. The IFA Medium-Term Fertilizer Outlook 2024–2028 expects global fertilizer demand to approach 200 million tonnes of nutrients annually. This pressure makes reliable output important. Ask suppliers to separate wet-feed capacity from finished-product capacity. A plant claiming 10 tonnes per hour may produce far less after drying and screening.
Inspect the process line in operation. Check feedstock receiving, fermentation temperature records, moisture control, odor management, granulation, and dust collection. Request three months of production data, laboratory certificates, maintenance logs, and customer acceptance records. FAO and ITPS soil assessments stress the value of organic matter and responsible nutrient management. Therefore, suppliers should explain carbon content, nitrogen stability, pathogen control, and contaminant testing.
Traceability matters. Each batch should connect to a feedstock source, processing date, operator, and test result. Ask whether the laboratory uses recognized methods, rather than unclear internal standards. Confirm electrical consumption, spare-part availability, installation support, and operator training. A lower purchase price can hide expensive downtime. This is often overlooked.
Be cautious with impressive projections. Feedstock variability can reduce throughput, especially during rainy seasons. I would test a supplier using the buyer’s actual material before signing. That step costs time. It may prevent years of inconsistent fertilizer quality.
2026 Top Organic Fertilizer Processing Plant Suppliers
Leading suppliers increasingly fall into four equipment categories: composting specialists, manure-processing integrators, pelletizing-line manufacturers, and liquid-fertilizer system builders. Composting plants typically provide shredders, windrow turners, forced-aeration floors, screens, and odor-control units. Manure processors focus on dewatering, fermentation, and pathogen-reduction systems. Pelletizing suppliers add dryers, mixers, pellet mills, coolers, and bagging machines. Liquid-fertilizer specialists usually supply macerators, dosing pumps, storage tanks, filtration, and automated filling lines.
Market selection should reflect feedstock, climate, labor, and local transport costs. FiBL’s World of Organic Agriculture 2024 report recorded 96.4 million hectares under organic management and approximately 4.5 million producers worldwide, based on 2022 data. That scale supports demand for flexible plants, not merely high-capacity machinery. The FAO’s fertilizer-related agricultural statistics also show why nutrient recovery and consistent application matter for soil productivity. In field evaluations, I would inspect moisture control, temperature records, screen accuracy, and emergency shutdown access before trusting output claims. Small details matter.
A practical supplier should provide test runs using the buyer’s actual manure, crop residue, or food waste. A laboratory sample is not enough. Pellet durability, dust levels, drying energy, and odor performance can change sharply after installation. Research reports often predict strong organic fertilizer market growth, but forecasts are not commissioning results. That distinction deserves attention. A lower-cost line may appear efficient, yet poor feedstock preparation can create blockages, uneven pellets, and expensive downtime. Suppliers with traceable data, operator training, spare-parts planning, and documented quality controls offer stronger long-term reliability.
| Supplier Category | Typical Feedstock | Core Processing Line | Main Equipment Capabilities | Typical Finished-Product Capacity | Suitable Product Forms | Key Selection Criteria |
|---|---|---|---|---|---|---|
| Compost-Based Fertilizer Plant Suppliers | Livestock manure, crop residues, food-processing waste, green waste | Pre-treatment → aerobic composting → crushing → screening → blending → granulation or packing | Windrow or in-vessel compost turners, shredders, chain crushers, rotary screens, batch mixers, granulators, bagging machines | 1–30 tonnes per hour, depending on the line configuration | Bulk compost, screened compost, powder, granules | Moisture control, odor management, feedstock variability, available curing area, screening accuracy |
| Manure Composting Equipment Suppliers | Cattle manure, poultry litter, pig manure, bedding materials | Mixing and moisture adjustment → forced or turned aeration → compost maturation → screening | Compost turners, fermentation tanks, aeration floors, manure mixers, belt conveyors, odor-control biofilters | 5–50 tonnes per hour of raw-material handling | Composted manure, powder fertilizer, pelletized or granulated fertilizer | Carbon-to-nitrogen balance, pathogen reduction, ammonia control, corrosion resistance, cleaning access |
| Organic Granulation Plant Suppliers | Mature compost, humic materials, manure compost, organic mineral blends | Crushing → proportioning → mixing → granulation → drying → cooling → screening → coating | Disc granulators, rotary drum granulators, double-roll extrusion granulators, rotary dryers, coolers, screeners, coating systems | 2–20 tonnes per hour of finished granules | Round granules, cylindrical granules, compacted granules, coated granules | Granule strength, size distribution, binder selection, drying energy, dust collection |
| Pelletizing Line Suppliers | Dry compost, peat substitutes, plant residues, organic meal materials | Drying or conditioning → fine grinding → mixing → pelletizing → cooling → screening → packing | Hammer mills, pin mills, paddle mixers, flat-die or ring-die pellet mills, counterflow coolers, pellet screens | 0.5–10 tonnes per hour of pellets | Cylindrical pellets, short pellets, slow-release organic pellets | Material fiber content, die-hole selection, pellet durability, energy consumption, moisture uniformity |
| Biofertilizer and Microbial Fertilizer Plant Suppliers | Sterilized organic carriers, compost extracts, molasses-based media, microbial cultures | Media preparation → sterilization or pasteurization → inoculation → controlled incubation → filling | Bioreactors, fermenters, sterilizers, clean filling machines, temperature-control systems, cold storage | 1,000–20,000 litres per batch for liquid products; 0.5–5 tonnes per hour for carrier-based products | Liquid inoculants, wettable powders, carrier-based powders, coated granules | Aseptic design, viable-cell preservation, pH control, temperature stability, contamination prevention |
| Liquid Organic Fertilizer Plant Suppliers | Compost extracts, plant hydrolysates, seaweed extracts, amino-acid solutions, animal by-product hydrolysates | Extraction or hydrolysis → filtration → blending → homogenization → storage → filling | Extraction tanks, hydrolysis reactors, decanter centrifuges, filter presses, storage tanks, filling machines | 1–30 tonnes per hour of liquid processing | Liquid concentrates, soluble extracts, foliar fertilizers, fertigation products | Solids removal, viscosity, pH stability, storage life, pump compatibility, filling accuracy |
| Vermicompost Processing Plant Suppliers | Pre-composted manure, crop residues, shredded plant material, organic household waste | Pre-composting → worm-bed processing → harvesting → screening → drying or packing | Vermibeds, pre-composting mixers, low-temperature dryers, rotary screens, conveyors, weighing and packing machines | 0.5–10 tonnes per hour of screened material | Fine vermicompost, screened castings, vermicompost blends, liquid extracts | Temperature and moisture protection, gentle material handling, screening size, biological activity preservation |
| Organic Waste Recycling Plant Suppliers | Municipal green waste, source-separated food waste, market waste, agricultural residues | Sorting → shredding → contaminant removal → composting or anaerobic digestion → refining | Bag openers, magnetic separators, shredders, trommel screens, composting tunnels, digesters, dewatering units | 5–100 tonnes per hour of incoming waste, depending on automation level | Compost, digestate solids, liquid fertilizer, soil amendments | Contamination removal, odor and leachate control, feedstock contracts, environmental permits, automation |
| Blending, Coating and Packaging System Suppliers | Finished compost, organic granules, mineral additives, micronutrients, biological additives | Ingredient dosing → batch or continuous blending → coating → weighing → bagging → palletizing | Loss-in-weight feeders, ribbon or paddle mixers, rotary coaters, automatic weigh fillers, sewing machines, palletizers | 5–60 tonnes per hour for blending; 10–30 bags per minute for common bagging formats | Bulk blends, 5–50 kg bags, big bags, coated granules | Dosing accuracy, mix uniformity, packaging format, dust control, traceability and batch reporting |
Note: Capacity ranges are representative engineering ranges and vary with feedstock moisture, bulk density, product formulation, equipment configuration and local operating conditions.
Choosing an organic fertilizer processing plant requires more than comparing quoted prices. A realistic cost review includes feedstock, drying energy, labor, packaging, testing, maintenance, freight, and minimum order quantities. Ask for a line-item quotation. A low price may hide unstable raw materials or weak quality controls. Request recent batch records, moisture results, nutrient analyses, and sample products before signing a contract. Field trials matter.
Certifications should match the product and destination market. Verify organic input approvals, ISO 9001 quality systems, ISO 14001 environmental systems, and laboratory accreditation where relevant. Check certificate numbers, issuing bodies, covered sites, product scopes, and expiration dates. A certificate alone proves little. Traceable records prove more. Suppliers should identify feedstock origins, processing temperatures, contamination controls, and storage conditions. Clear documentation supports regulatory reviews and customer confidence.
Sustainability needs measurable evidence. Examine energy use per ton, water consumption, odor controls, dust collection, renewable power, and packaging materials. Ask whether the plant reuses process heat or recovers rejected batches safely. Site visits can reveal details that documents miss, such as leaking conveyors or uncovered stockpiles. Delivery reliability also matters; inspect capacity, backup equipment, lead times, and communication practices. I would score suppliers using weighted criteria, not instinct alone. Even careful assessments can miss seasonal feedstock changes. Recheck performance after the first three shipments.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift